Routing examples
Two worked examples of a six-operation routing in Phasio, one for powder bed printing and one for FDM printing, with every operation setting.
Available to manufacturers on the Factory Floor plan
These examples show how to set up the operations behind a simple 3D printing routing in Phasio, from the initial part queue through post-processing and quality control to completion. Use them as a reference when you set up your own operations and assign them to your processes and post-processing options. See Set up your routing.
Both examples use six operations and the same tools: a download and upload of nested or sliced files at Printing, grouping by material (and colour) for batch handling, and naming strategies that keep a group's name as it moves through post-processing.
Powder bed printing
This routing manages powder bed printing while keeping clear visibility and control over each production stage.
Routing sequence
- Waiting for Nesting: initial backlog management.
- Printing: active production with build preparation.
- Post-Printing: essential post-production processes, such as cooling and depowdering.
- Black Dye: optional finishing.
- Quality Control: final inspection and validation.
- Completed: routing completion and order fulfilment.
Operation configuration
| Operation Name | Sequence | Group Name Prefix | Step Type | Build Constraint | Step Naming Strategy | View Type | Final Station |
|---|---|---|---|---|---|---|---|
| Waiting for Nesting | 0 | Waiting | Base | None | Always Rename | Part | False |
| Printing | 1 | Build | Upload Bill of Parts | Material | Always Rename | Group | False |
| Post-Printing | 2 | Batch | Base | Material | Inherit from Previous Step | Group | False |
| Black Dye | 3 | Dye-Batch | Base | Material and Color | Inherit from Previous Step | Group | False |
| Quality Control | 4 | QC-Batch | Quality Control | None | Inherit from Previous Step | Part | False |
| Completed | 5 | Finished | Base | None | Always Rename | Part | True |
Operation details
Waiting for Nesting holds the backlog of parts that have been scheduled for production.
- Uses the Base step type, so parts must be progressed manually.
- Parts wait here until they are ready to move to Printing.
Printing: when parts enter this operation, the Upload Bill of Parts step type lets you download each group of same-material parts (as a ZIP or CAMSPEC file) for nesting, then upload the nested .3mf file to stage the parts.
- With the Group view type, these parts appear as consolidated groups. To give a group a custom name, right-click it in the Backlog group view and select Rename, or click the Rename group (pencil) icon on the build screen.
Post-Printing: parts entering this operation are grouped by material for efficient processing. The Inherit from Previous Step naming strategy keeps the group name when the moved set of parts is unchanged; a partial split gets a new group number under the old prefix. This keeps build identification consistent through essential post-production steps such as cooling and sandblasting.
Black Dye is an optional finishing operation where parts are grouped by material and colour to keep the dye treatment consistent. The Inherit from Previous Step naming strategy keeps group names from previous stages when the group is unchanged; a partial split gets a new group number under the old prefix.
Quality Control has no grouping constraints. The Inherit from Previous Step naming strategy maintains traceability: when the group is unchanged its name carries through; a partial split gets a new group number under the old prefix.
Completed is the final stage of the routing.
- Parts arriving here are automatically renamed with a "Finished" prefix using the Always Rename naming strategy.
- This operation is the final station (Final Station = True), marking the end of production.
- As parts reach this stage, the order's Production tab shows the completed and total quantity of each part, for example 3 / 4. The Completed operation in the Backlog lists work completed in the last 30 days. Click Load more to see older work.
- Nothing is progressed out of the final station; the build screen shows "This is the final operation — nothing leaves this step."
- Use this station to represent open boxes or staging areas until the entire order is ready for shipment.
Part progression and filtering
When moving parts from one operation to the next on the progress screen, you can filter by Customer, Dispatch Date, Visits Operations, Volume, Area, Height, Width and Length to plan builds efficiently. Parts can also be grouped by order and sorted by dispatch date or volume. The Visits Operations filter is especially useful for grouping parts that share identical post-processing, which supports efficient planning and resource allocation.
Part progression flow
-
From the order's Production tab, use Create work orders to schedule parts into production. Each part enters the routing at Waiting for Nesting once its work order is created.
-
On the progress screen of Waiting for Nesting, production teams download parts grouped by material with Download Parts on the lane heading into Printing.
-
Build preparation is completed offline using nesting software.
-
Upload Bill of Parts on the same lane takes the nested
.3mffile and stages its parts into a new group. Click Proceed to move the group into Printing. -
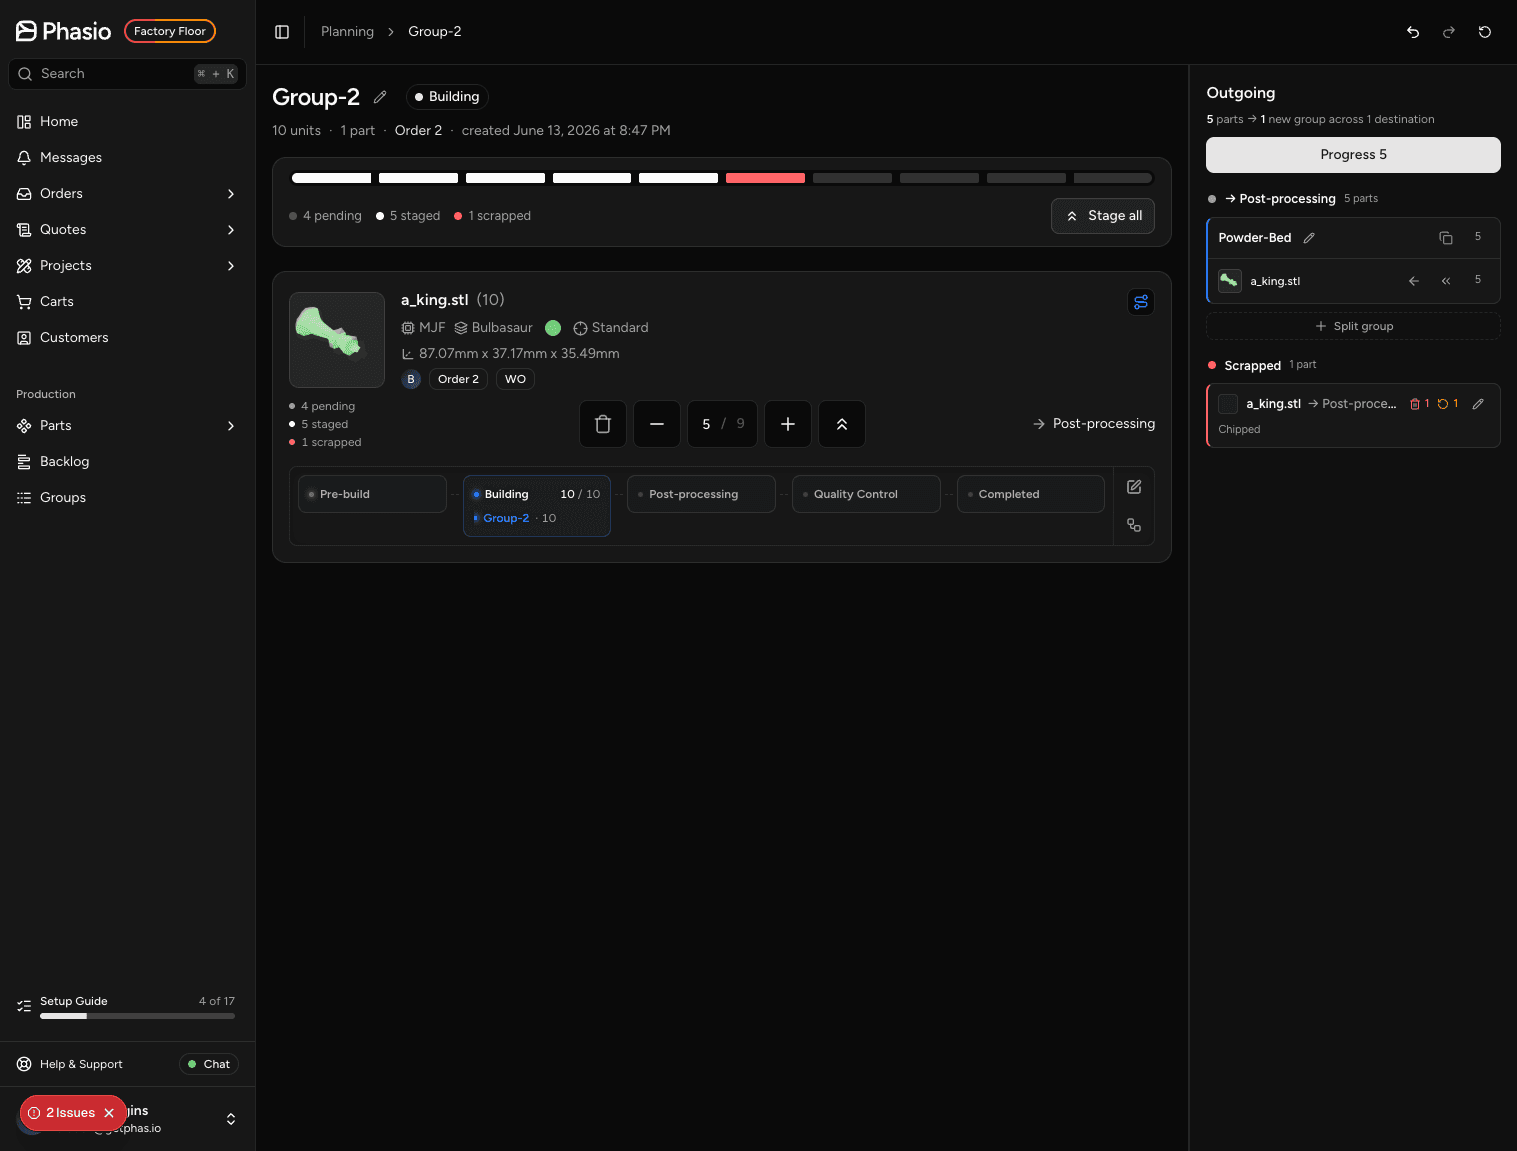
On the build screen, stage parts per destination, name the outgoing group, and click Progress N to commit the move without leaving the page.
-
Repeat for each following operation, Post-Printing, Black Dye (if applicable) and Quality Control, using the same build screen flow.
At any operation you can scrap individual parts from the build screen and optionally queue a replacement quantity. The replacement tops up the existing work order at its first operation.
Benefits
This example shows how operation configuration can improve production efficiency while keeping the flexibility to meet diverse manufacturing needs and optional processing steps:
- Material-based grouping lowers error rates and reduces setup time.
- Batch processing via
.3mfuploads streamlines high-volume production and simplifies build preparation. - Flexible routing supports different customer requirements and custom routings.
- Real-time tracking gives visibility of parts throughout production.
FDM printing
This routing manages FDM printing while keeping clear visibility and control over each production stage, and accommodates the needs of filament-based printing.
Routing sequence
- Waiting for Slicing: initial backlog management.
- Printing: active production with print preparation.
- Post-Printing: essential post-production processes, such as part removal and support removal.
- Polishing: optional surface finishing.
- Quality Control: final inspection and validation.
- Completed: routing completion and order fulfilment.
Operation configuration
| Operation Name | Sequence | Group Name Prefix | Step Type | Build Constraint | Step Naming Strategy | View Type | Final Station |
|---|---|---|---|---|---|---|---|
| Waiting for Slicing | 0 | Queue | Base | None | Always Rename | Part | False |
| Printing | 1 | Print Job | Upload Bill of Parts | Material and Color | Always Rename | Part | False |
| Post-Printing | 2 | Batch | Base | Material and Color | Inherit from Previous Step | Part | False |
| Polishing | 3 | Polish-Batch | Base | Material and Color | Inherit from Previous Step | Part | False |
| Quality Control | 4 | QC-Batch | Base | None | Inherit from Previous Step | Part | False |
| Completed | 5 | Finished | Base | None | Always Rename | Part | True |
Operation details
Waiting for Slicing manages the backlog of parts that have been scheduled for production.
- Uses the Base step type, which has no operational effect, so parts must be progressed manually.
- Parts are only moved out of this station; no processing happens here.
Printing: when parts move into this operation, the Upload Bill of Parts step type lets you download parts (as a ZIP or CAMSPEC file) grouped by material and colour.
- After preparing the sliced print job, parts can be progressed individually or as a group. To stage a group, upload the exported
.3mffile or a.csvbill of parts with Upload Bill of Parts. G-code files are not accepted. - In most cases parts move individually, as a print typically holds a single part, unless a full build plate is prepared.
Post-Printing supports the post-processing steps immediately after printing.
- Parts are grouped by material and colour for efficient batch handling.
- The Inherit from Previous Step naming strategy preserves custom job names given during Printing.
- Jobs stay clearly identified through key post-printing processes such as removing parts from the build plate and removing support structures.
Polishing is an optional finishing operation where parts are grouped by material and colour, so identical finishing treatments are processed together. The Inherit from Previous Step naming strategy keeps job names as parts are finished to improve print quality and appearance.
Quality Control: parts moving into this operation have no grouping constraints. The Inherit from Previous Step naming strategy maintains traceability by keeping job names from earlier stages during final inspection and validation.
Completed is the final stage of the routing.
- Parts arriving here are automatically renamed with a "Finished" prefix using the Always Rename naming strategy.
- This operation is the final station, marking the end of production.
- Use this station to represent storage until the entire order is ready for shipment.
Scheduling a work order
Parts enter the routing when a work order is created with Create work orders on the order's Production tab. See Work orders.
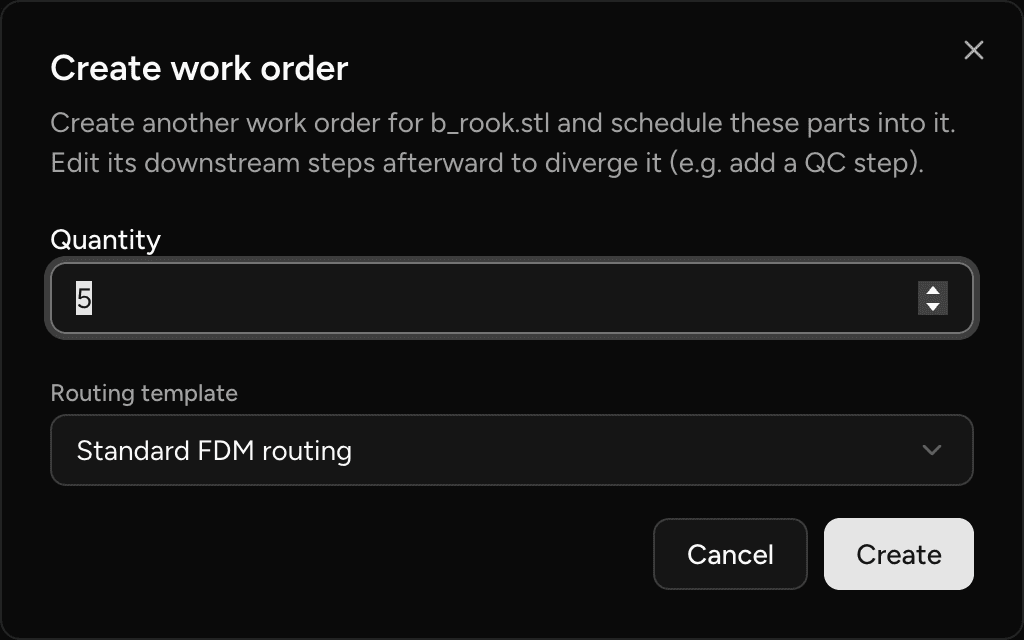
If you have set a default routing template for the part, it is applied automatically. Without a default template, the work order's routing is derived from your current process configuration.
Part progression and filtering
When moving parts from one operation to the next on the progress screen, you can filter by Customer, Dispatch Date, Visits Operations, Volume, Area, Height, Width and Length to plan builds. Parts can also be grouped by order and sorted by dispatch date or volume. The build screen has no filters.
Build screen
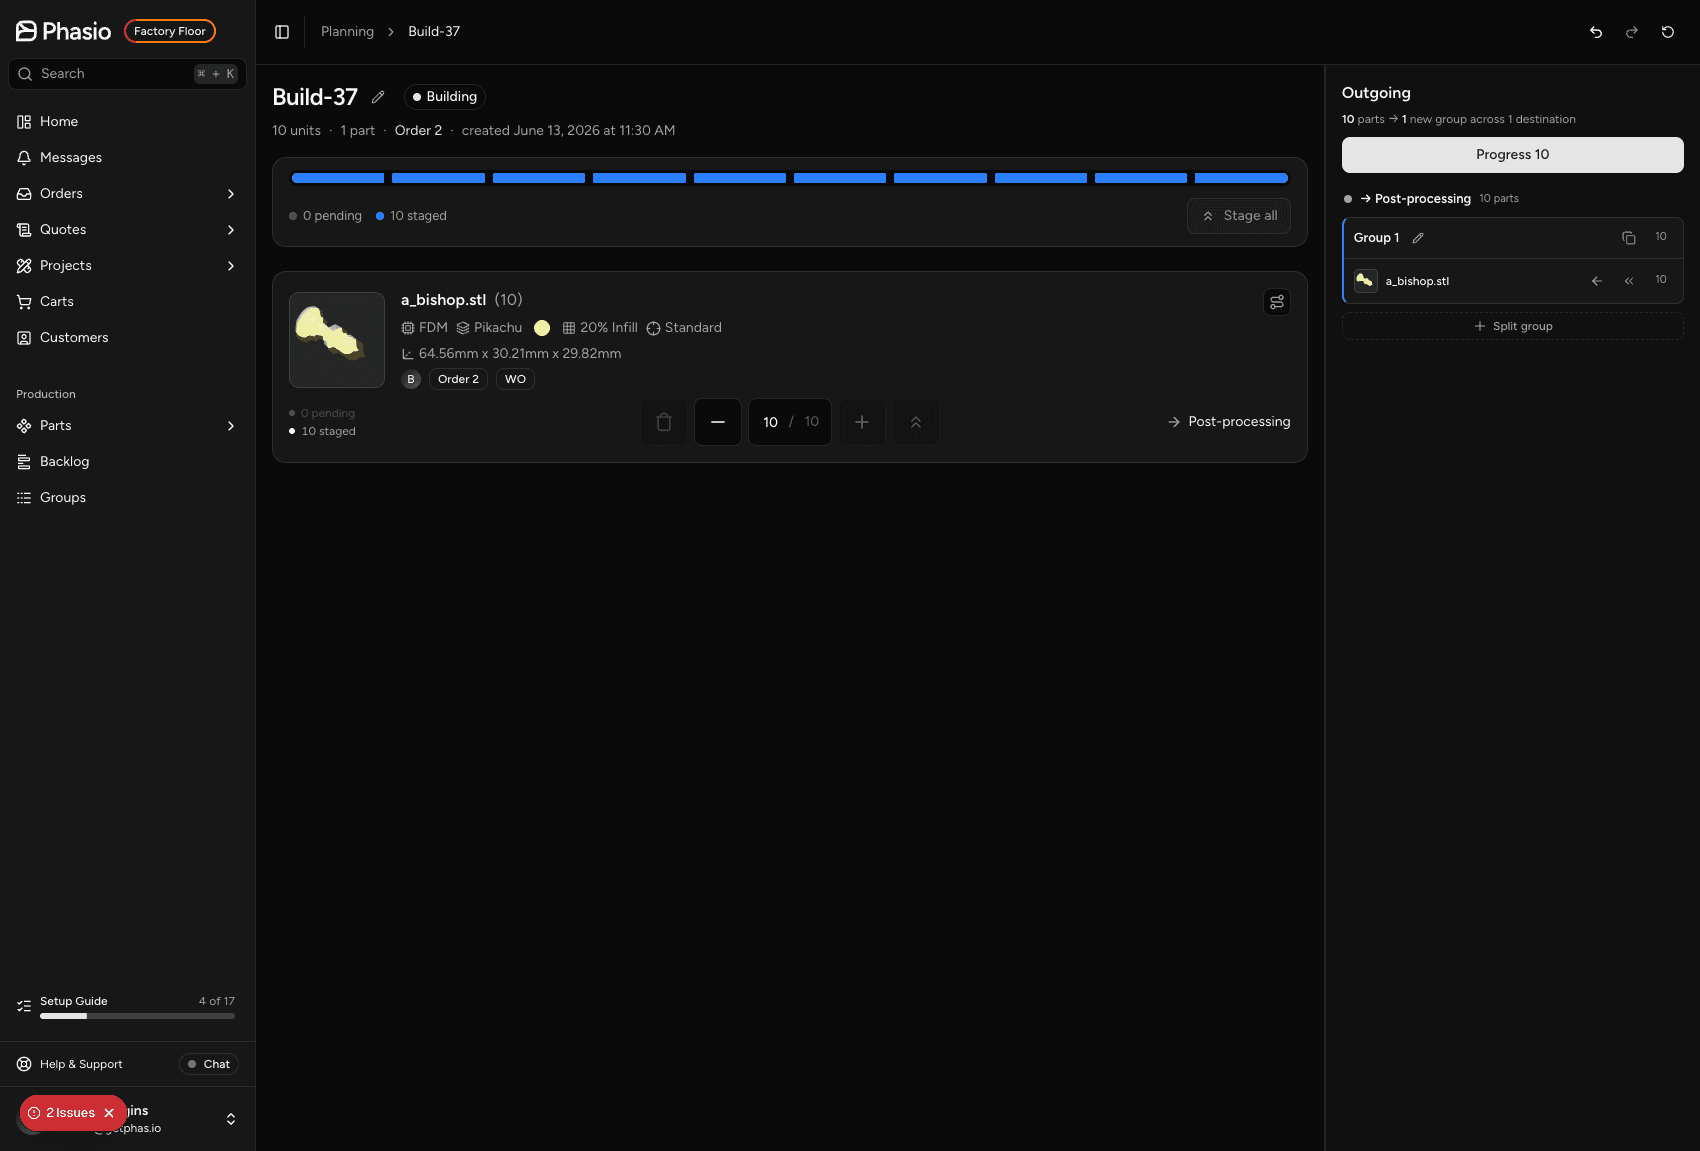
Open a group to reach the build screen. From here, operators stage parts per destination, name the outgoing group, and commit the move with Progress N. See Build screen.
Scrap management
At any operation, individual parts can be scrapped. Give a scrap reason for quality tracking and optionally schedule a replacement quantity; the replacement is queued on the work order automatically. See Scrap parts.
Part progression flow
- Create a work order for the part from the order's Production tab. Parts land at Waiting for Slicing.
- On the progress screen of Waiting for Slicing, use Download Parts on the lane heading into Printing to download parts grouped by material and colour.
- Prepare the print job offline with slicer software.
- Upload the exported
.3mffile or a.csvbill of parts with Upload Bill of Parts on the same lane. Phasio stages the matching parts into a group. Click Proceed to move them into Printing. - Move parts manually through Post-Printing, Polishing and Quality Control.
- Parts reaching Completed are renamed with the "Finished" prefix.
Benefits
- Material and colour grouping minimises filament changes and reduces setup time.
- Flexible batch processing supports both single-part and multi-part print jobs.
- Individual part tracking gives precise visibility, well suited to FDM's typically smaller batch sizes.
- Clear visibility of the routing makes sure support removal, finishing and downstream operations are handled properly.
Last updated on
Routing templates
Create, approve, set a default for and retire routing templates on a part specification, and require approved templates before production.
Scheduling
Set up your resources and operation timings, then use the Schedule page to see when every work order finishes and test changes before you apply them.